Non-destructive inspection method for detecting cracks, pores, and other surface defects in process equipment before they turn into contamination risks, microbiology issues, or costly shutdowns.


WHAT IS CRACKS & PORES INSPECTION
Non-Destructive Method to Find Defects Your CIP System Cannot Clean
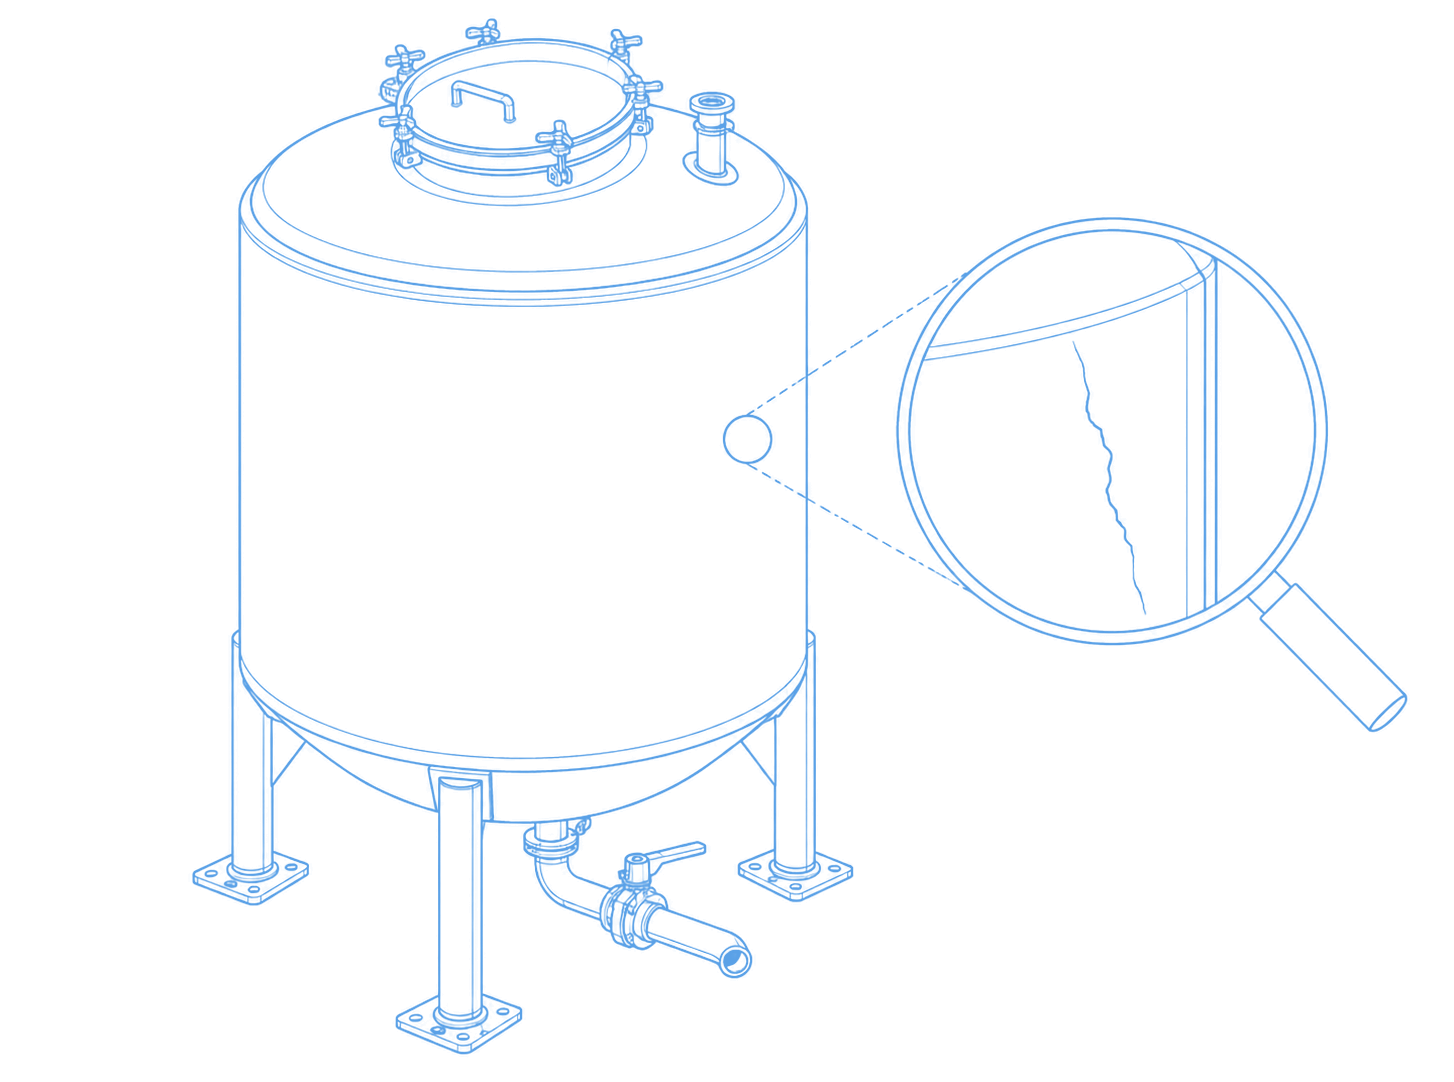
Cracks & Pores Inspection uses dye penetrant testing as a non-destructive hygienic surface inspection for detecting surface-breaking cracks, pores, and micro-fissures on process equipment, tanks, welds, and pipelines. Liquid penetrant inspection, including food-safe fluorescent penetrant testing where applicable, helps reveal discontinuities that may be difficult to detect visually and can compromise cleanability.
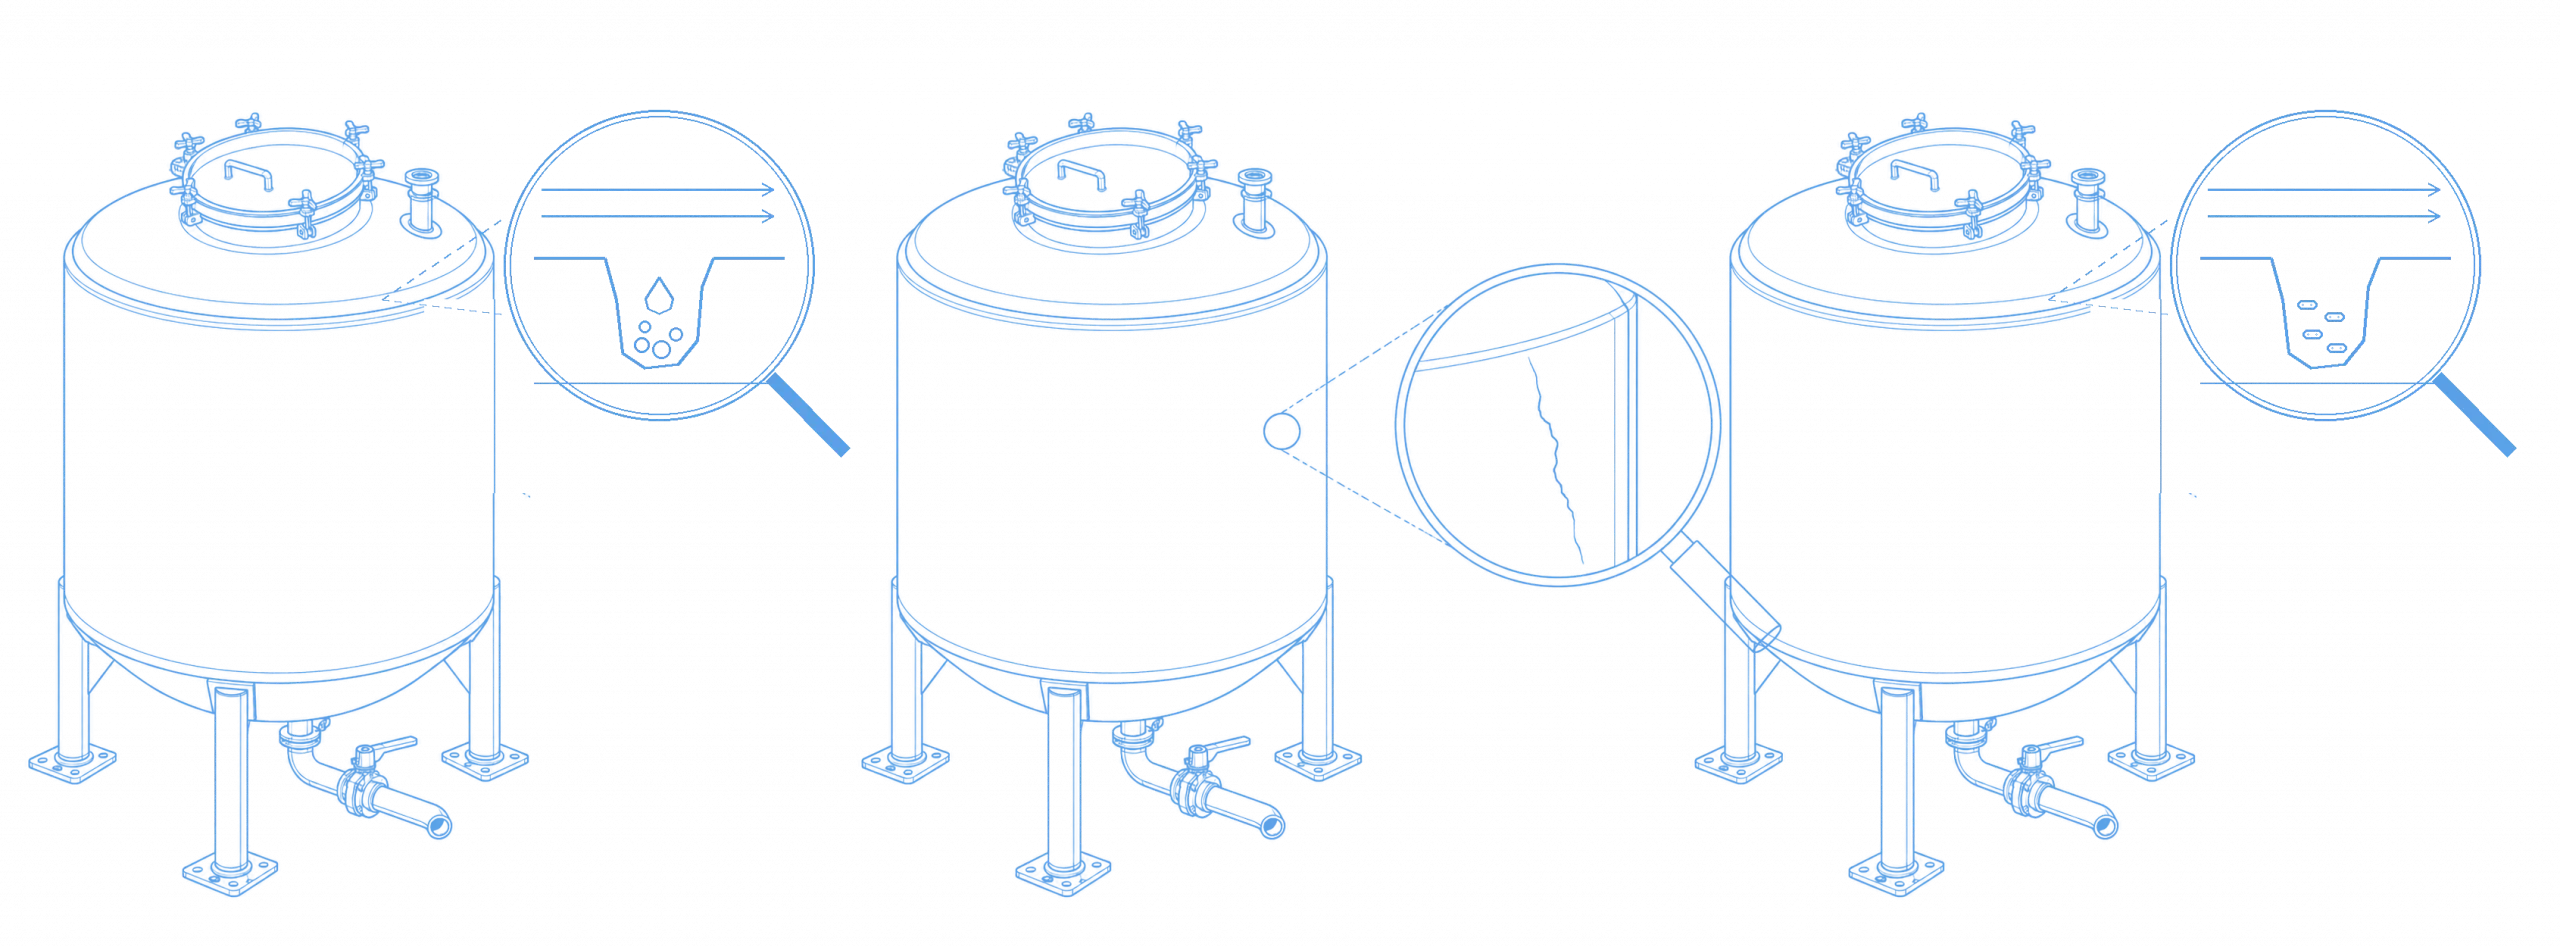
Surface defects are critical in hygienic production because they create micro-zones that standard CIP cleaning cycles cannot reach. Residual product, moisture, and bacteria accumulate in these voids, forming what are commonly known as bacteria traps. Cracks & Pores Inspection helps identify these defects before they compromise product safety or trigger audit findings.
WHY CRACKS & PORES INSPECTION MATTERS
Cracks, pores, and damaged surface zones can become hidden hygiene risks. If they remain undetected, they may contribute to contamination, microbiological issues, repeated cleaning problems, audit findings, and unplanned downtime. Integrity testing helps identify these weak points early and gives engineering teams a basis for action before they affect production.

Microscopic defects harbour bacteria that survive CIP cycles. Detection prevents contamination of liquid food products.

A crack that cannot be cleaned by CIP is a permanent contamination risk. Testing identifies where CIP protocols are physically limited.

EHEDG and HACCP require documented evidence of equipment surface integrity. Testing provides the inspection report your audit team needs.

Detecting a crack before a production run is cheaper than managing a contamination event, product recall, or unplanned shutdown.

Finding defects during planned maintenance prevents unplanned line shutdowns caused by recurring contamination or weld failures.

Applicable to any stainless steel or non-porous surface — tanks, pipes, heat exchangers, valves, fillers, and packaging equipment.
WHEN THIS SERVICE IS NEEDED
This inspection is relevant when there are concerns about cracks, pores, fatigue damage, corrosion, weld condition, or hard-to-explain hygiene deviations. It is also useful after repair work, grinding, repeated cleaning issues, microbiological concerns, or before critical quality reviews.
01
Every new weld joint in product-contact areas should be tested before commissioning. Post-weld testing is required for EHEDG-compliant installations.
02
If a weld was ground or a surface repaired, chemical etching followed by penetrant testing is required — grinding may have smeared micro-cracks closed without eliminating them.
03
Equipment qualification protocols for CIP systems should include integrity testing to confirm that the cleaned surface is free of defects that would invalidate the cleaning validation.
04
When ATP swab tests, rinse water analysis, or product testing reveals unexplained contamination despite correct CIP execution, integrity testing can locate the bacteria trap causing the problem.
05
HACCP and EHEDG guidelines recommend periodic inspection of product-contact surfaces in high-risk zones — particularly heat exchangers, weld-intensive vessels, and fillers.
06
Pre-audit integrity inspection ensures that equipment surface condition is documented and defensible — avoiding findings related to undetected surface defects or bacteria trap zones.
DEFECTS WE DETECT
Standard visual inspection misses defects smaller than 0.5 mm and those hidden beneath surface oxides or residues. Cracks & Pores Inspection is designed to reveal surface-open defects that can become hygiene, quality, or reliability risks.
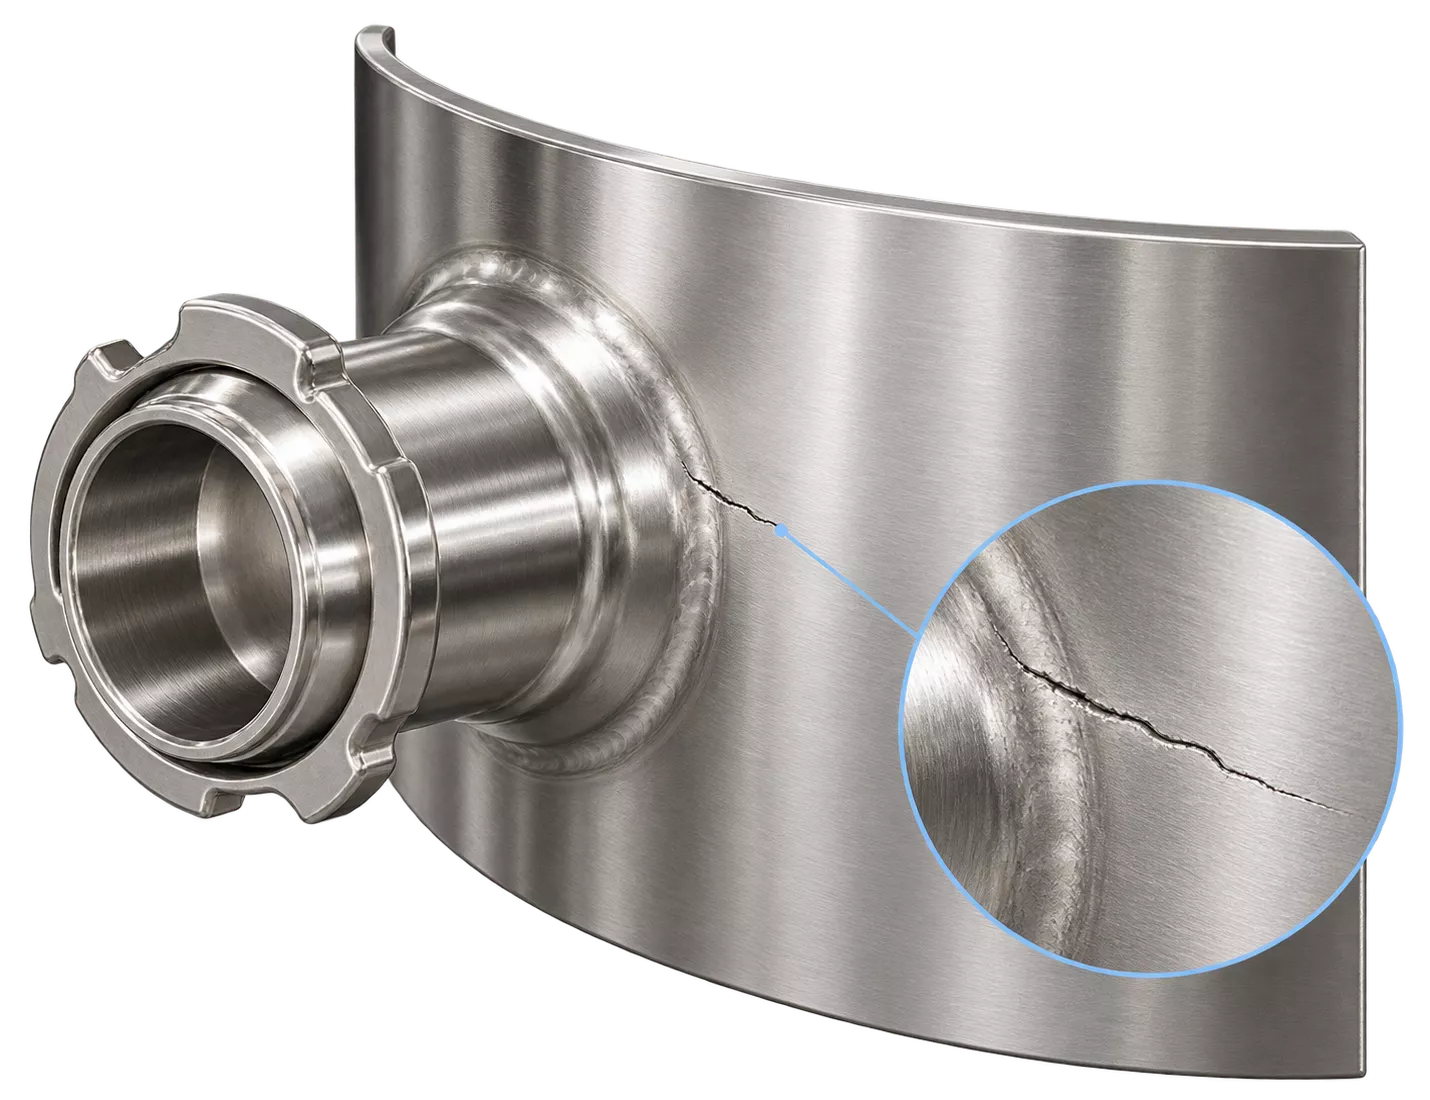
Fatigue cracks from thermal cycling, mechanical stress, or weld cooling. Often invisible to the naked eye but detectable with fluorescent penetrant under UV light.
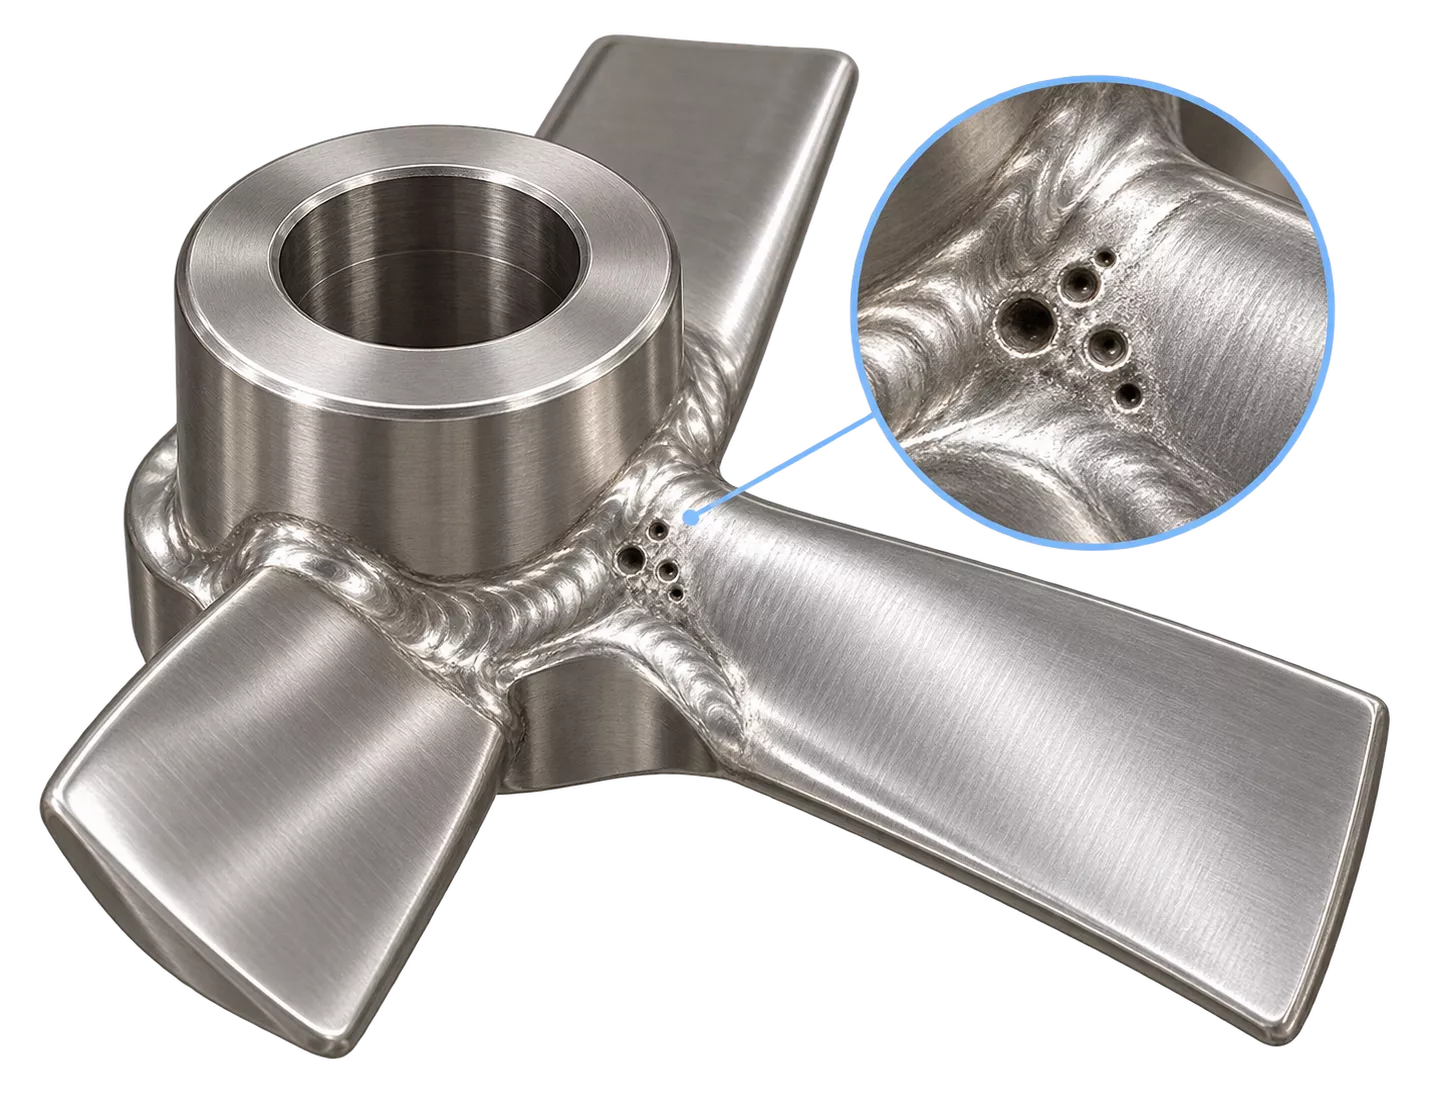
Gas pockets trapped during welding, casting, or forming. Each pore is a potential bacteria trap that CIP chemicals cannot penetrate and rinse.
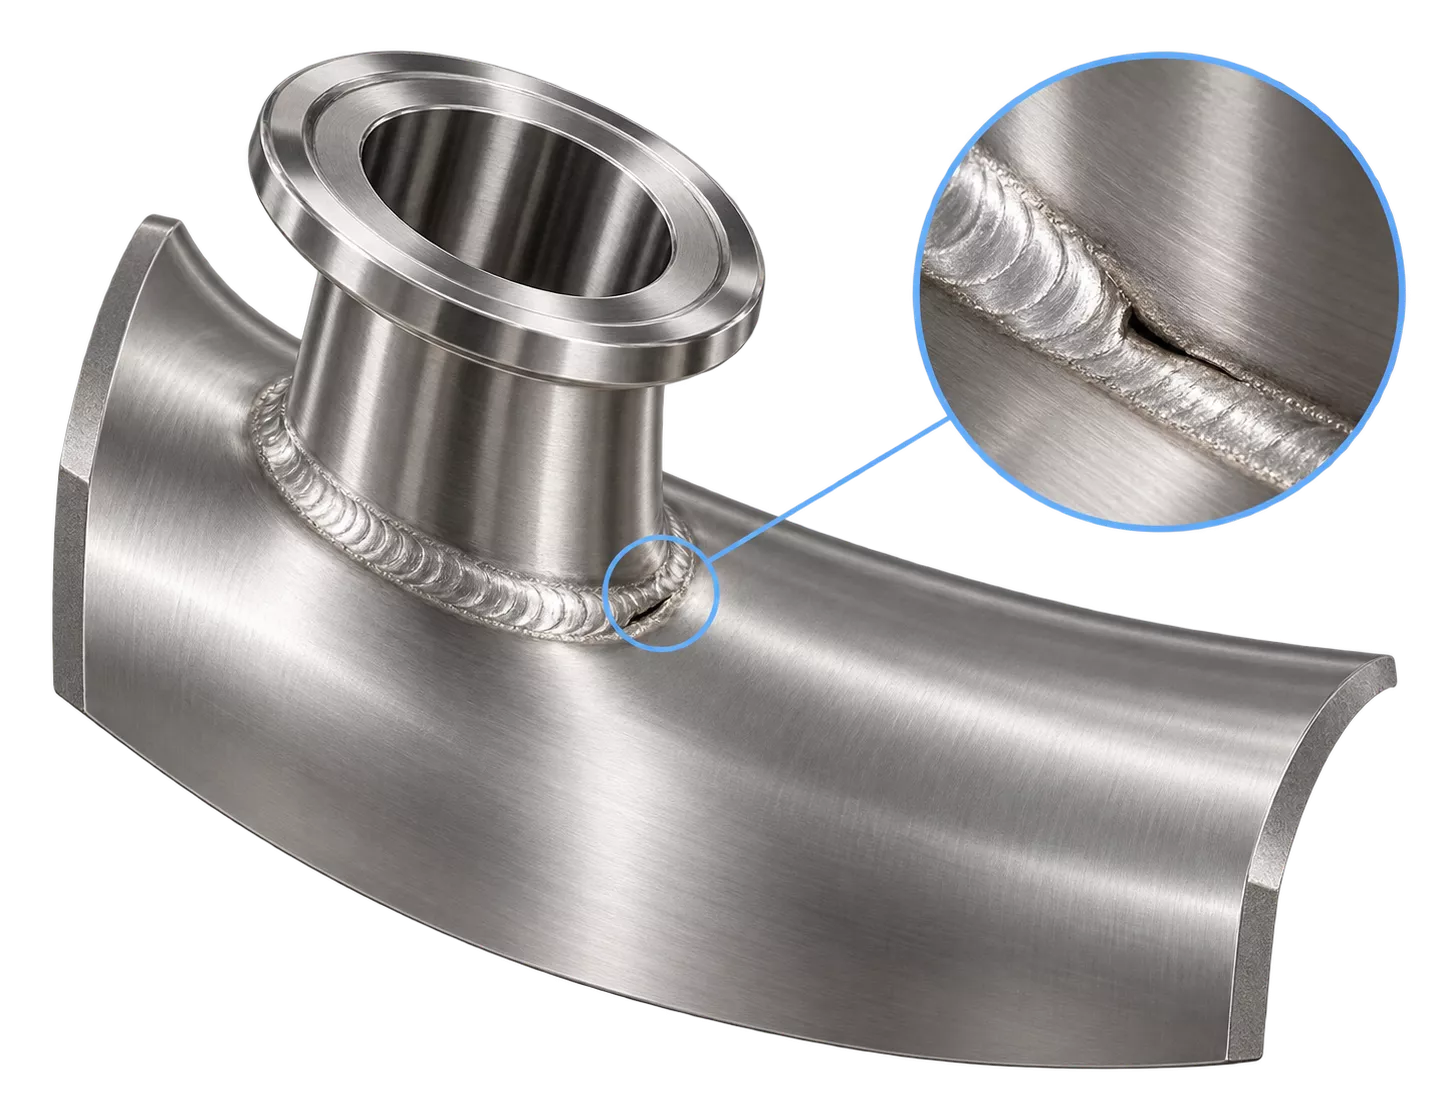
Incomplete fusion, undercut, or micro-cracks at weld toes and heat-affected zones — the most common location of integrity failures in stainless steel equipment.
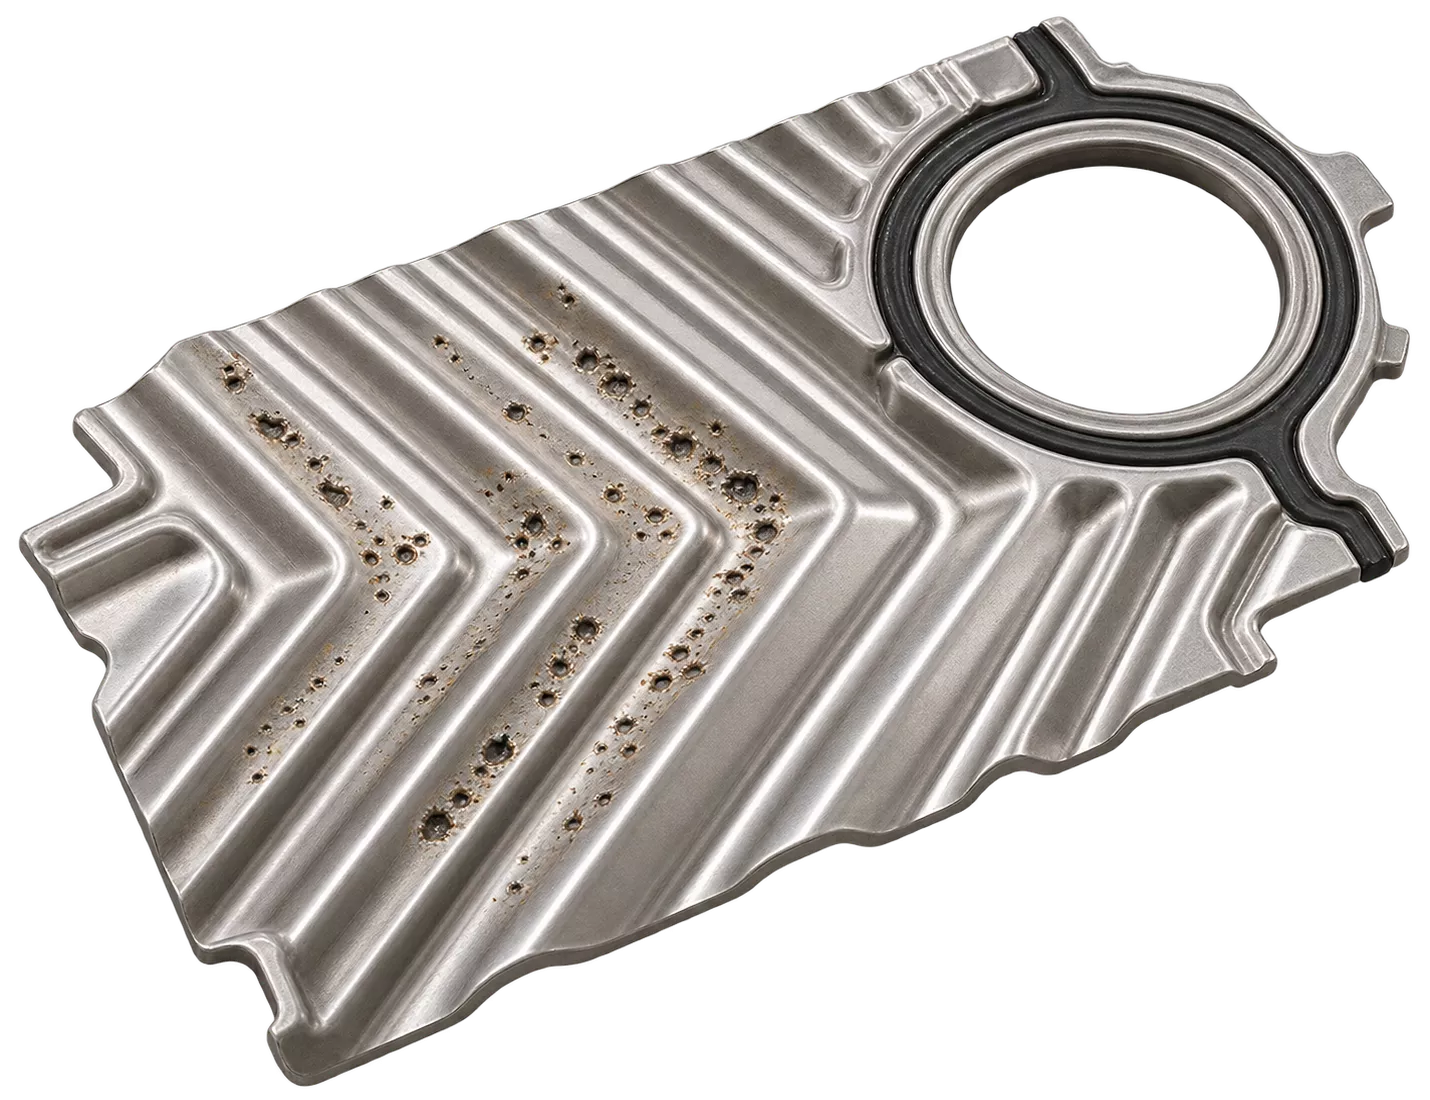
Early-stage pitting from chloride attack or mechanical damage. Detected before pits grow into through-wall defects or structural failures.
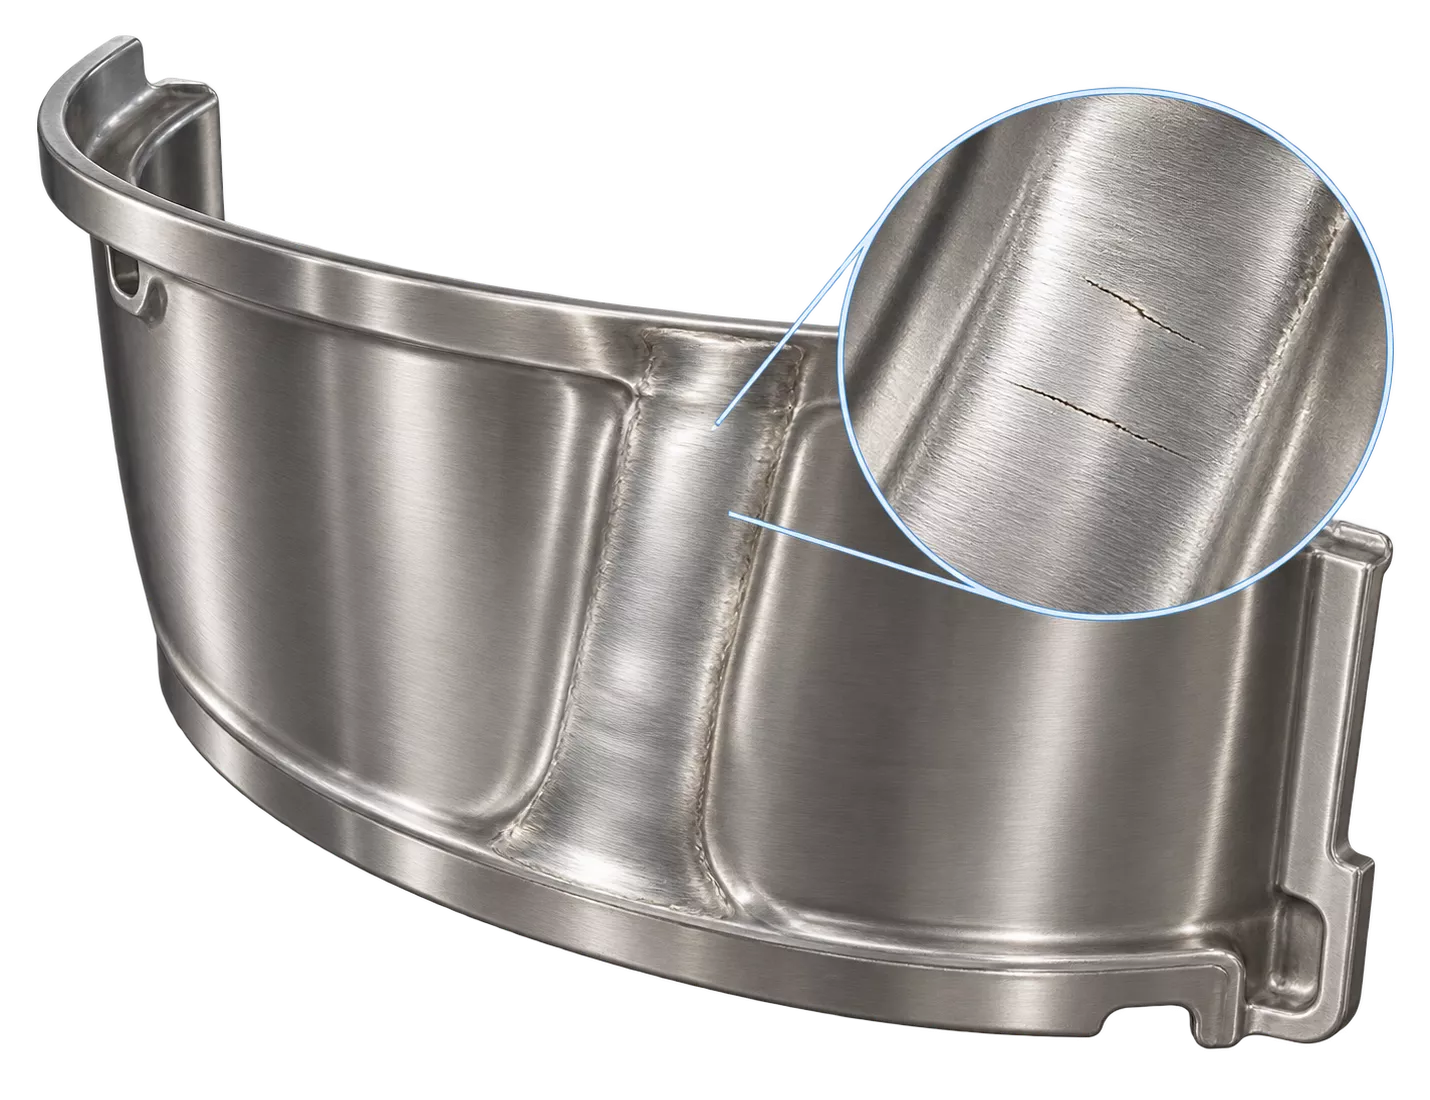
After grinding or polishing a weld repair, micro-cracks are sometimes “smeared” closed. Chemical etching combined with penetrant testing reopens and reveals these hidden defects.
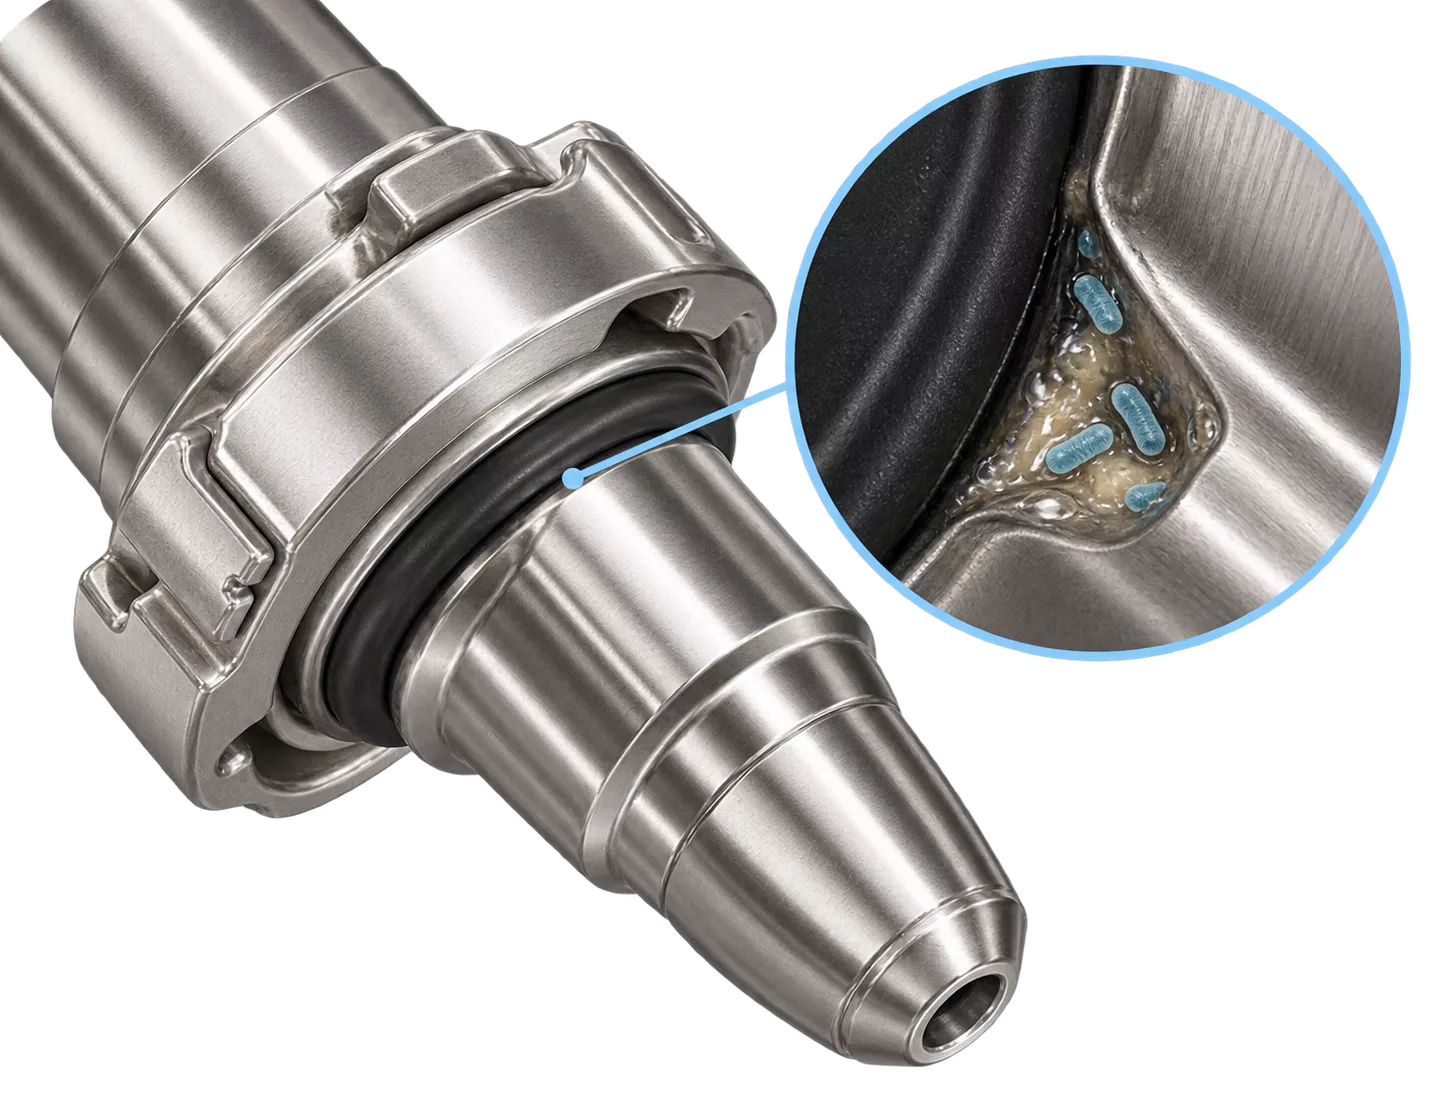
Any surface void that CIP chemistry cannot flush — gasket interfaces, crevices, overlapping surfaces — identified for corrective action or design correction.
TYPICAL EQUIPMENT
Testing can be applied to multiple types of process equipment where surface condition matters for hygiene, product safety, and reliable operation.Cracks & Pores Inspection is suitable for both tanks and other contact surfaces in process lines.
HOW THE TEST IS PERFORMED
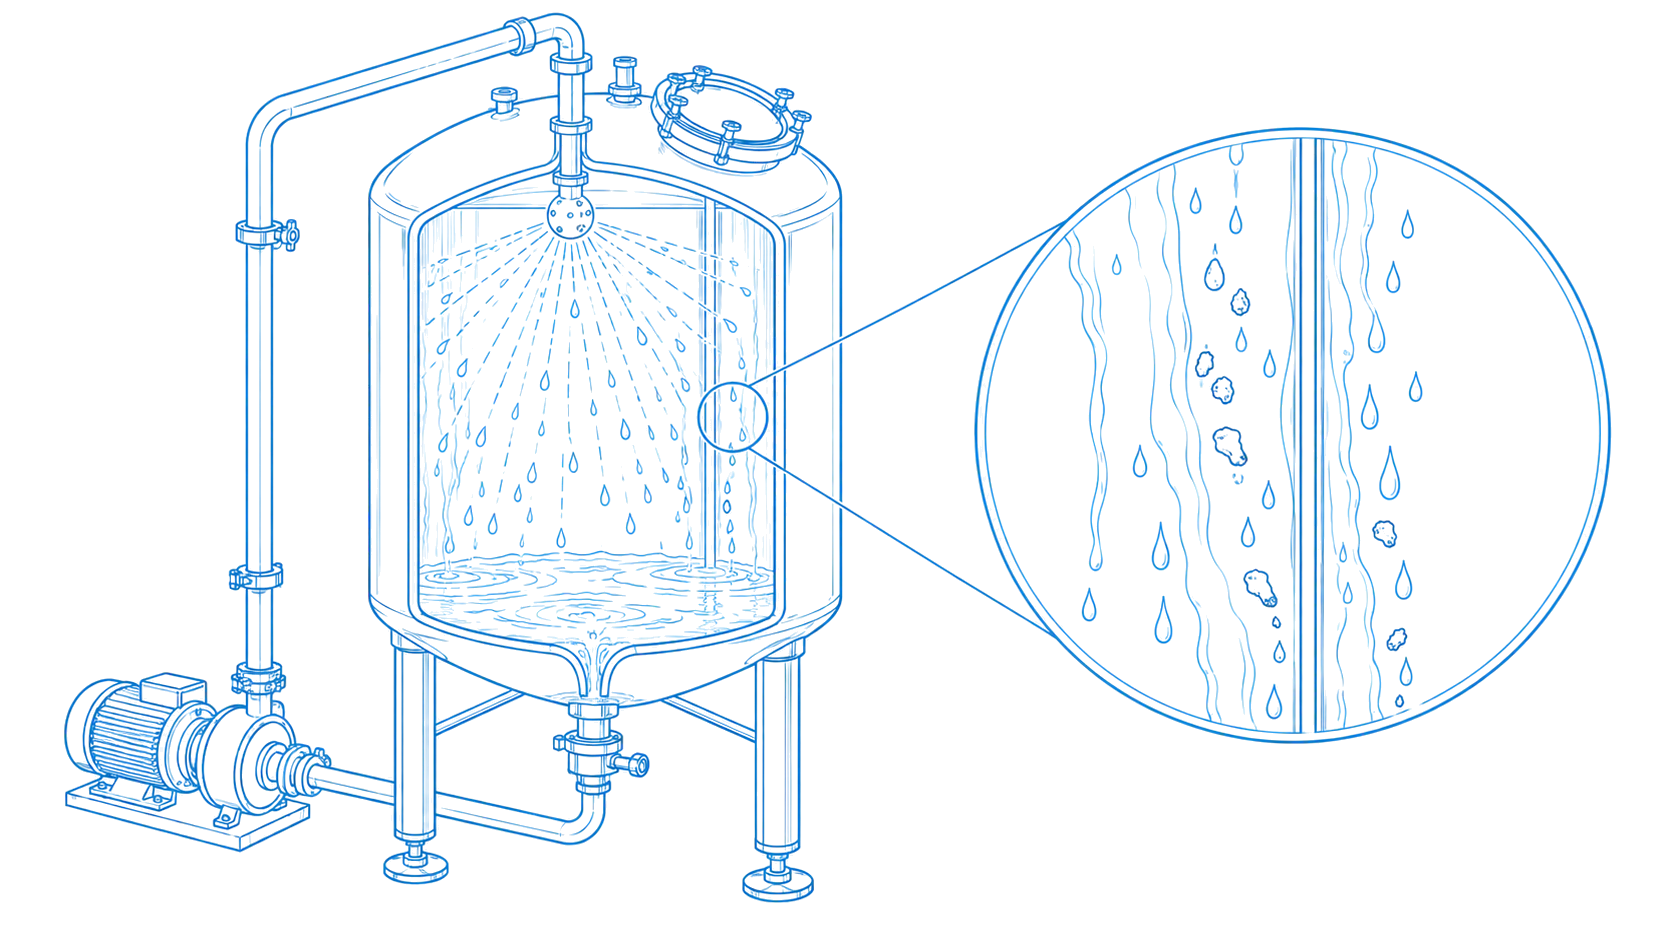
01
All dirt, grease, oil, and product residues are removed from the equipment surface. A thorough CIP procedure is applied to ensure a perfectly clean substrate. Any contamination at this stage can mask defects or produce false results.
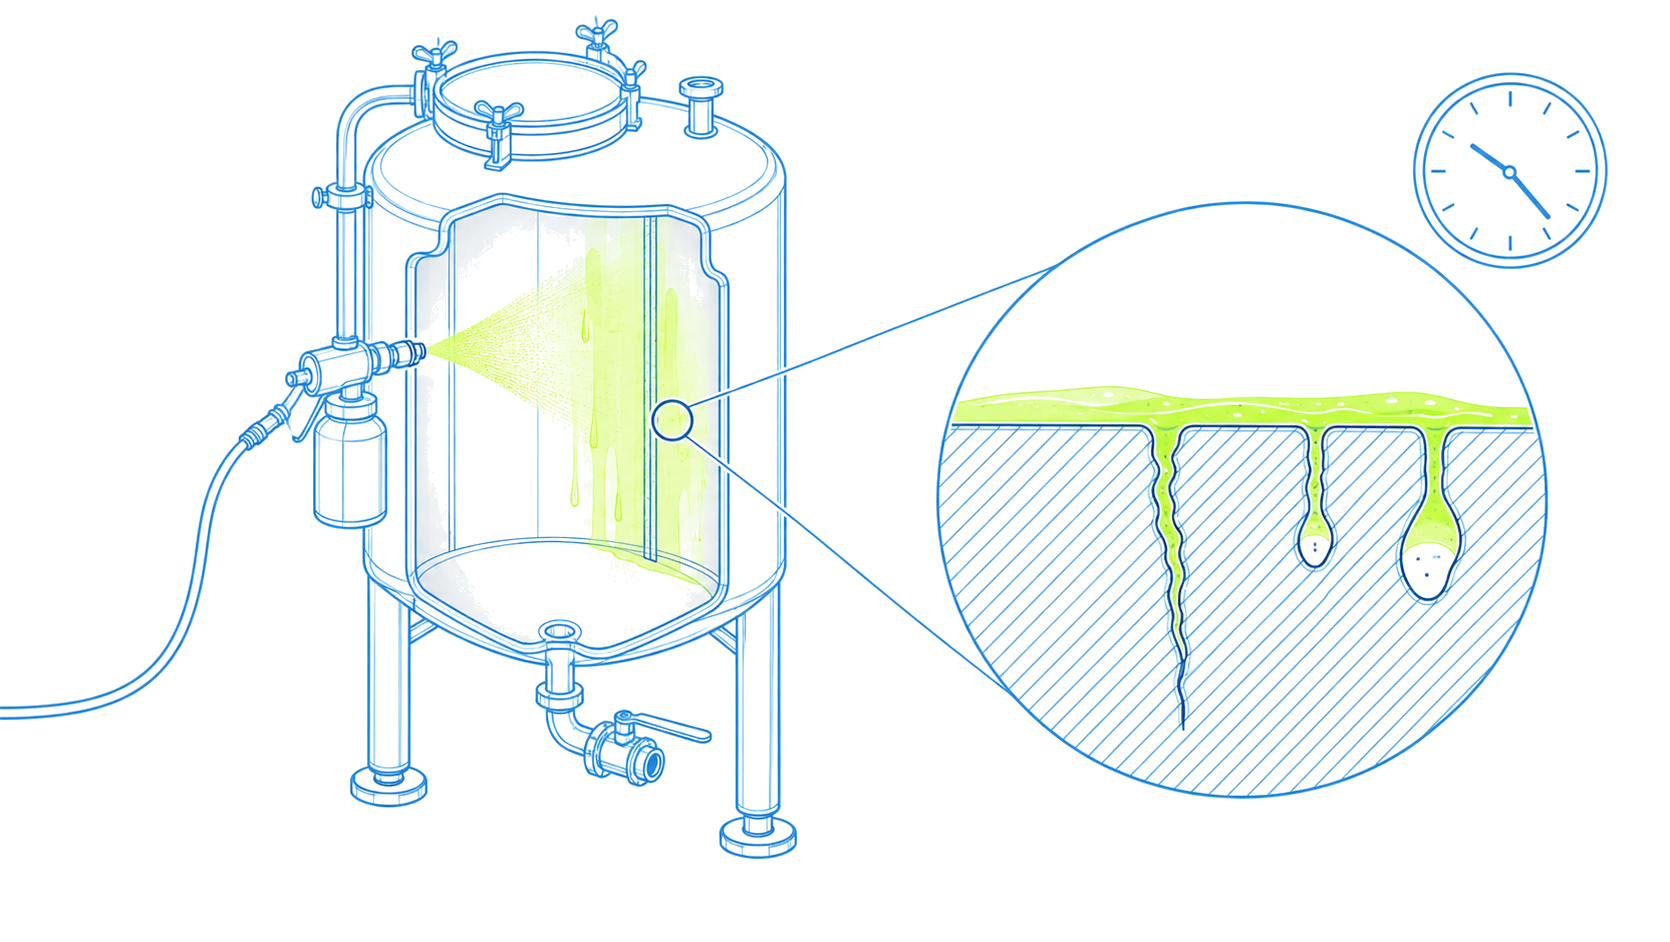
02
A food-grade fluorescent penetrant is applied to the surface. This low-viscosity liquid seeps into cracks, pores, and surface discontinuities through capillary action. A controlled dwell time allows the penetrant to fully enter all defects.
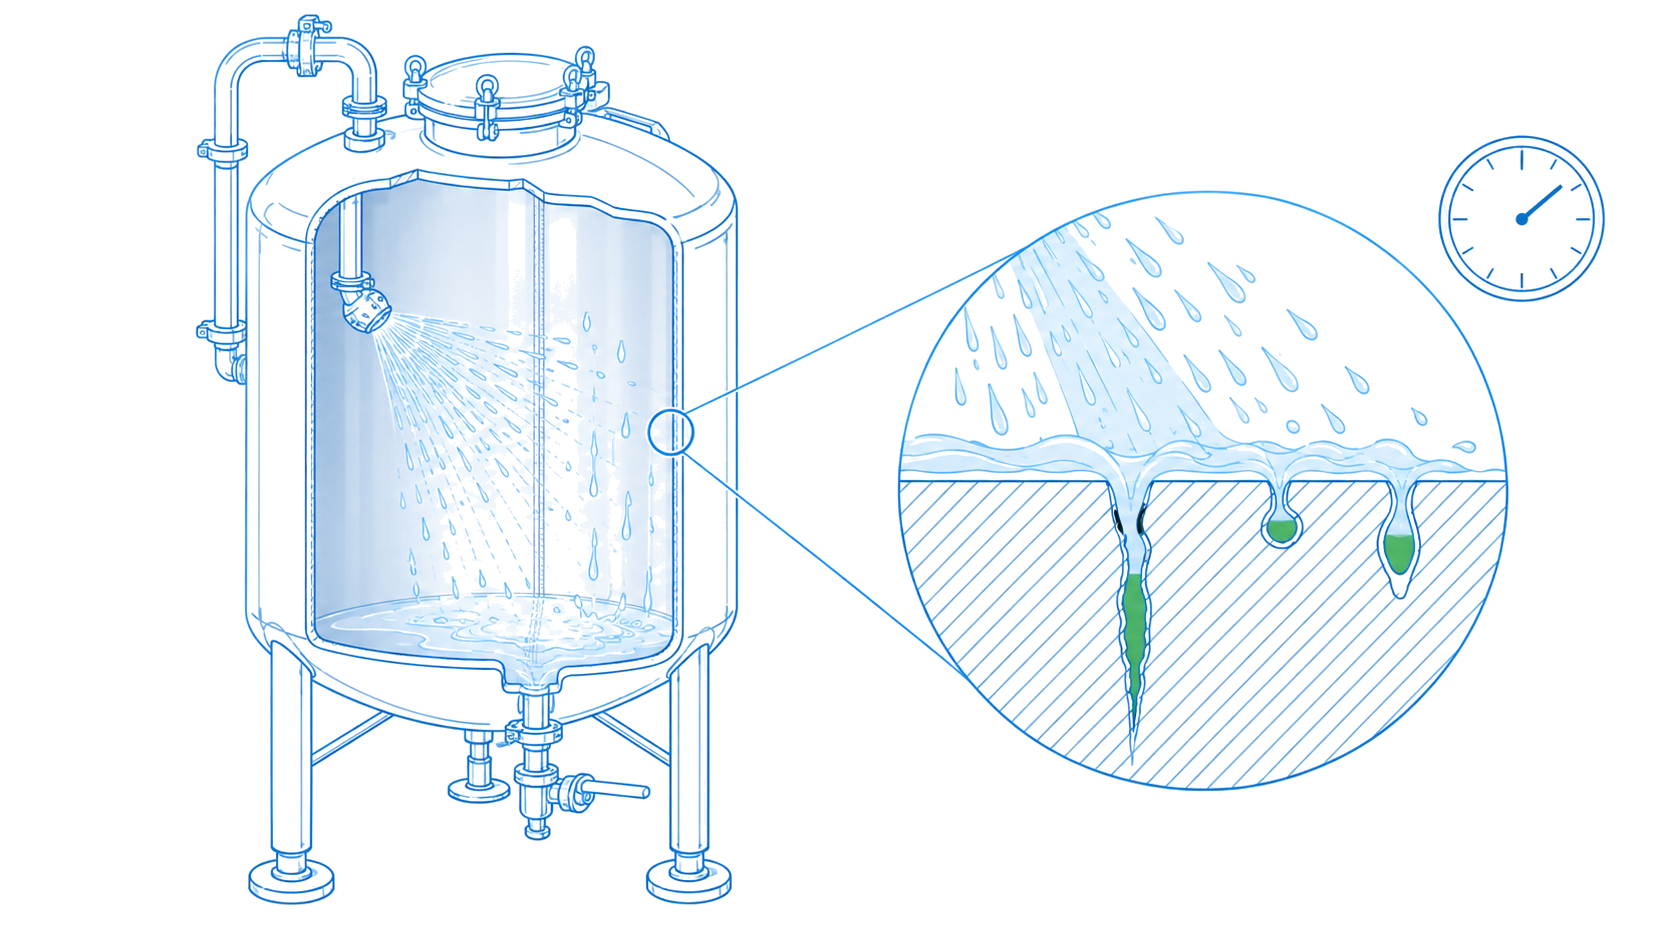
03
After the dwell time, excess penetrant is removed with cold water washing. Penetrant trapped inside defects remains in place. A detection time follows to allow contrast to develop before the UV inspection begins.
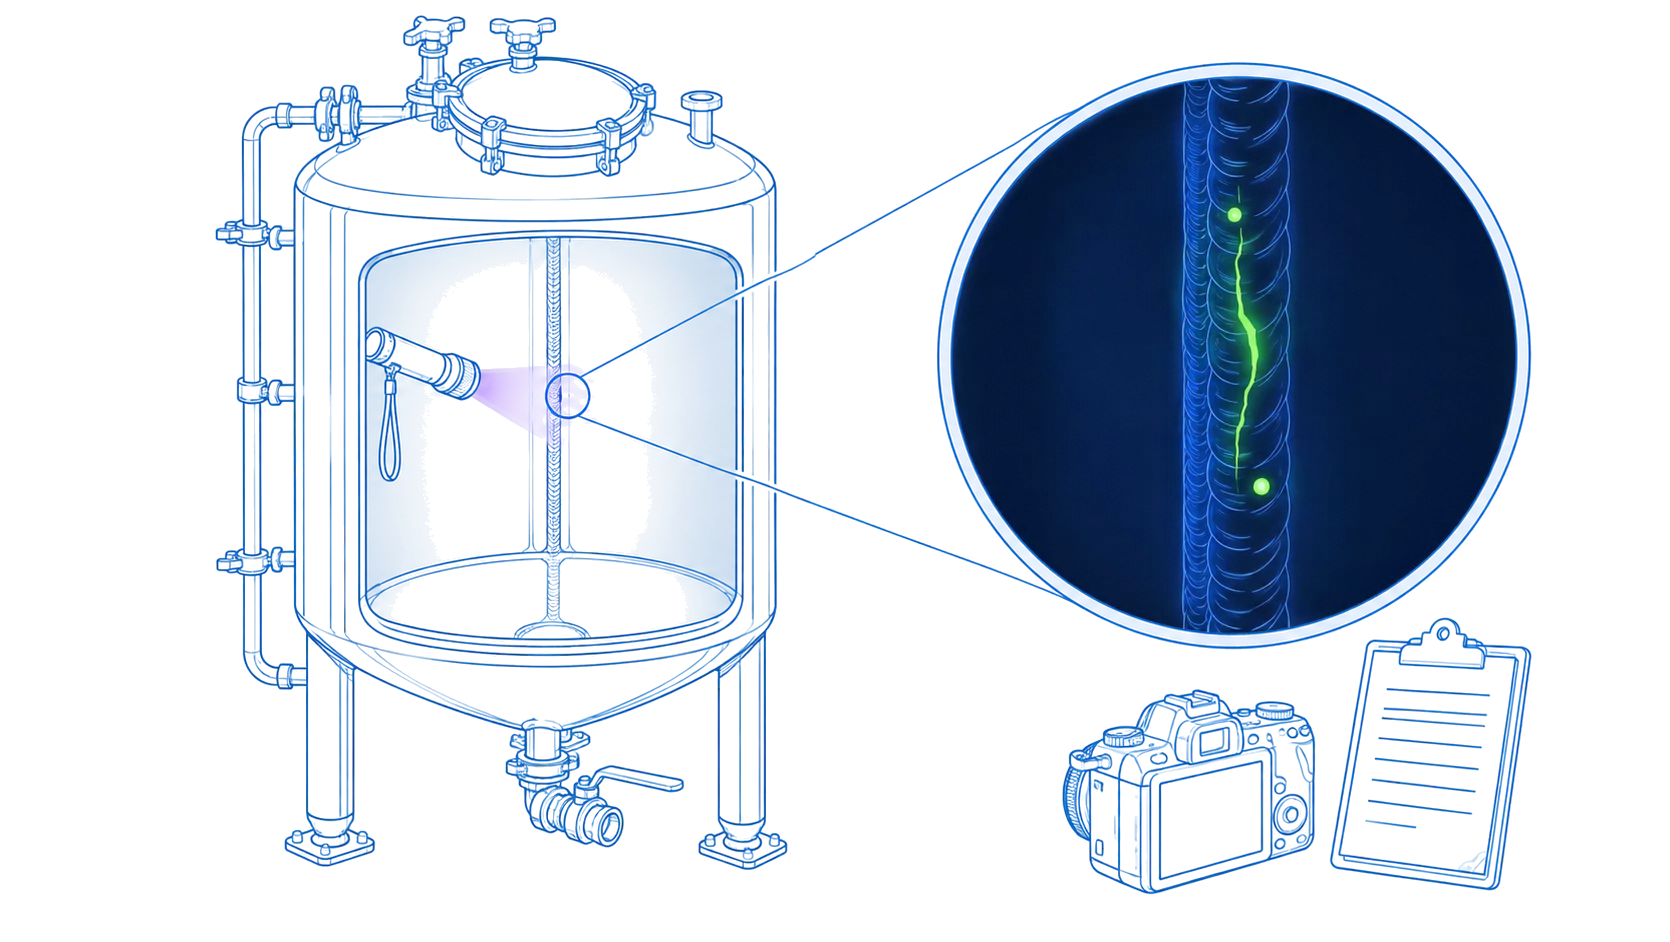
04
The surface is examined under UV irradiation in low-light conditions. Fluorescent indications glow brightly, making cracks and pores immediately visible. All findings are documented with photographs and a detailed inspection report.
HOW THE SERVICE IS DELIVERED
The inspection method is only one part of the service. In practice, plants also need a clear service workflow: identifying what should be inspected, preparing the equipment, carrying out the test, documenting findings, and defining follow-up actions. This makes the service easier to plan and more useful for quality, engineering, and production teams.
01
Define which equipment, tanks, welds, or internal surfaces require inspection based on risk, history, or hygiene concerns.
02
Confirm that equipment is properly cleaned and, where relevant, assess whether additional preparation such as etching is required after grinding or repair.
03
Perform the penetrant test according to the inspection sequence and inspect critical zones under UV conditions.
04
Record visible indications, defect locations, and relevant observations with photo evidence where applicable.
05
Define whether repair, additional inspection, repeat testing, or hygiene-risk follow-up is needed.
WHAT YOU GET
The value of testing is not limited to defect detection alone. After the inspection, your team receives a detailed report that documents the inspected equipment, the tested zones, visible defect indications, and the main observations from the inspection. This helps engineering, quality, and production teams review the condition of critical surfaces, prioritise repairs or follow-up checks, and keep a clear record of findings for internal decision-making.

ES
ZS
IL
DI
LG
SO
RS
STANDARDS IN USE
The method is aligned with recognized penetrant testing principles.
Non-destructive testing of welds
Penetrant testing
Acceptance levels
WHY CIP EXPERTS
01

We know CIP processes in detail and understand how hygiene issues develop in process equipment — and how to investigate them correctly.
02

We stay available before, during, and after the service to help the customer move from inspection findings to practical next steps.
03

We adapt the testing scope to the complexity of the project, the equipment involved, and the specific needs of each customer.
04

Every inspection ends with a clear, detailed report that shows the findings, highlights the problem areas, and outlines recommended actions.
FAQ
Is it safe to use penetrants in food production equipment?
For the food industry, food-safe, non-toxic, and biodegradable penetrants are required. Often, water-washable fluorescent indicators are preferred because they are easier to remove with water, minimizing the risk of residual chemical contamination.
Which critical zones of the tanks must be inspected?
In addition to welds, penetrant testing allows for an inspection of the entire internal surface and base material for fatigue cracks, porosity, or corrosion. This is critical for preventing the formation of “bacteria traps”—microscopic voids that cannot be reached by standard Clean-in-Place (CIP) systems, which could otherwise compromise product sterility.
Is special surface preparation required before testing?
Cleaning: CIP procedure is typically used to remove product residues.
Etching: If mechanical grinding was performed to smooth a weld or repair, chemical etching is often required to reopen micro-cracks that may have been “smeared” or closed by the metal-working process
Related Pages
Explore complementary inspection, testing, and qualification services for a complete CIP validation scope.
Tell us about your equipment and production environment.
We will confirm scope, access requirements, and available dates within 1 business day.
Thank you for your request!
Our team will contact you soon to discuss your project and the next steps.
Request Sent
Thank you for contacting CIP Experts. Our manager will contact you within one business day.
